CNC BENDING / FORMING
With CNC forming and bending, the usual failures are a wrong angle on the second bend, scrap on a repeat order, and a part that needed three setups.
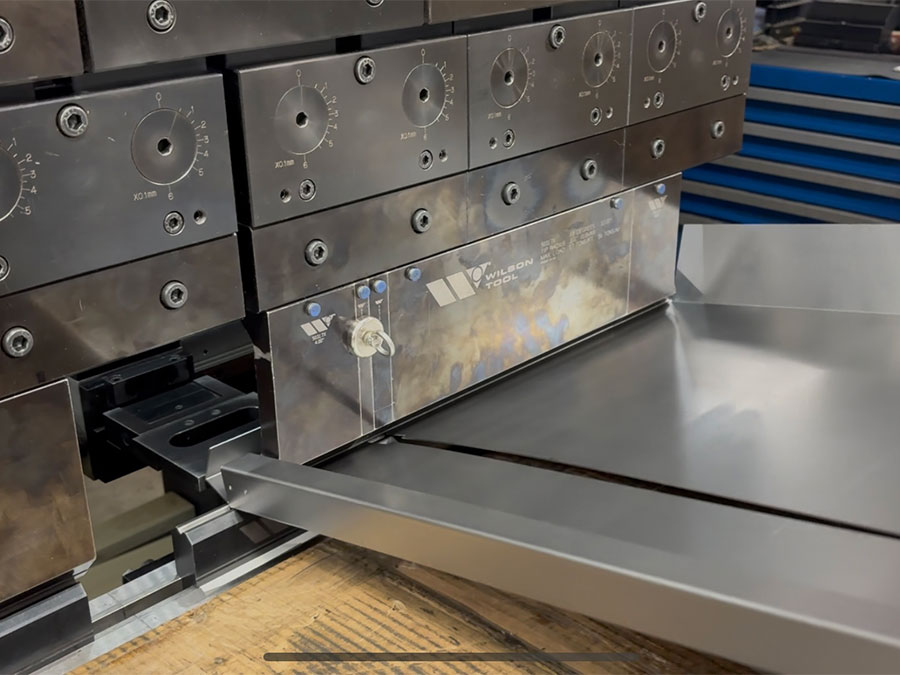
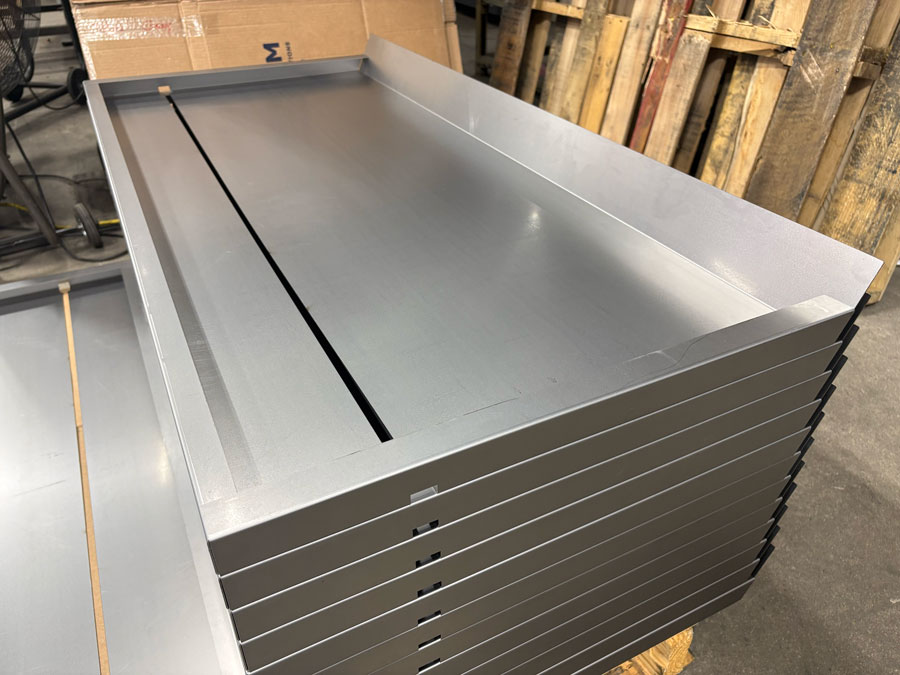
Multi-stage bends are done in one setup, so the part is not rehandled between angles. Standard hold is ±0.5° angular and ±.005 inches dimensional. That is what keeps a chassis, bracket, or cover from being refitted at your assembly line.
- We form complex, multi-bend pieces using multi-axis CNC press brake bending to complete advanced angles.
- Manual sheet metal bending increases lead times and the risk of scrap on high-volume orders. With our machinery, we deliver highly efficient operations to reduce lead times and pass cost savings on to the customer.
FAQ


EQUIPMENT
- TOYOKOKI HYB 1253 WIN II-2010-120'' Max Bed Length-125 Metric Tons
- Mitsubishi Windows XP 3D touch screen control- 9 Axis-Backgauge-Auto Thickness Sensing - Double Wedge Crowning-Auto Ram Tilt - Auto Backgauge Tilt
- DIAMOND(MITSUBISHI) BH13530-2018-120” Max Bed Length-135 Metric Tons
- Mitsubishi Windows XP 3D touch screen control- 9 Axis-Backgauge-Auto Thickness Sensing - Double Wedge Crowning-Auto Ram Tilt - Auto Backgauge Tilt
- DIAMOND(MITSUBISHI) BB6020-2019-83” Max Bed Length-55 Metric Tons Servo Electric
- Mitsubishi Windows XP 3D touch screen control- 9 Axis-Backgauge-Auto Thickness Sensing -Auto Ram Tilt - Auto Backgauge Tilt
- Dries & Krump, 90 Ton, 120" Long, Equipped with Front & Back
- All Steel, 50 Ton, 96" Long, Equipped with Front & Back Air Operated Micrometer Gauging
- Brakes, 20 to 30 Ton, 48" to 72" Long

Need a quote before placing your order?
ALL CAPABILITIES

FIBER LASER CUTTING
CNC BENDING / FORMING

CNC / TURRET PUNCHING

WELDING / SPOT WELDING

FABRICATION SERVICES